

The Shandong Fengxiang integrated poultry farming and processing project has an annual slaughter capacity of 80 million. During the planning stage, the site layout was developed around the existing terrain and facilities to connect live-bird receiving and finished-product warehousing with the existing plant infrastructure.
The poultry slaughtering, by-product processing, cut-up, and quick-freezing areas were carefully planned as separate functional zones. Personnel and material flows, as well as dirty and clean areas, were also fully separated to support food hygiene and safety from the start of the production process.

MOON-TECH developed a highly automated production workshop with closely coordinated processing stages, from bird hanging, slaughtering, and bleeding through automatic grading, cutting, and leg removal. The integrated slaughtering and cut-up line helps improve overall production efficiency.

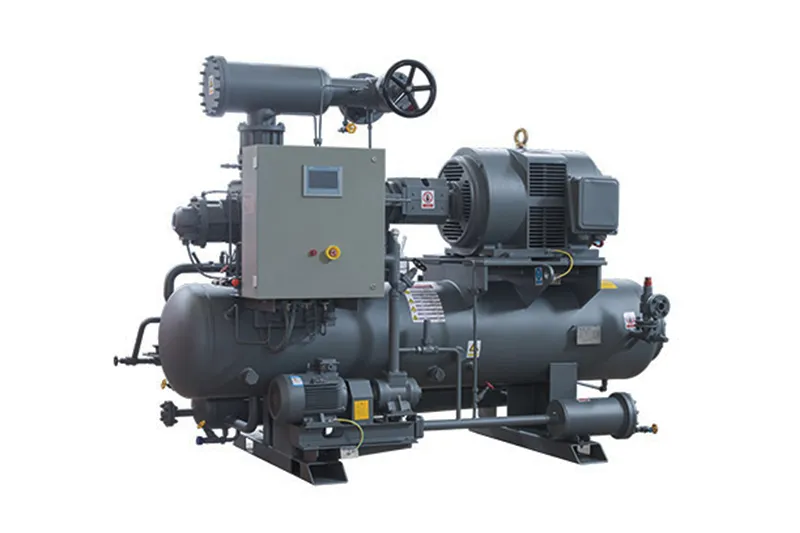
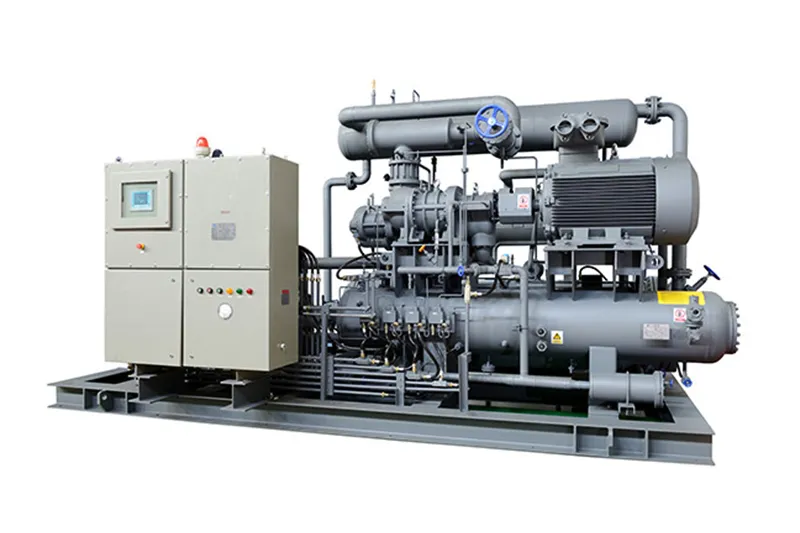
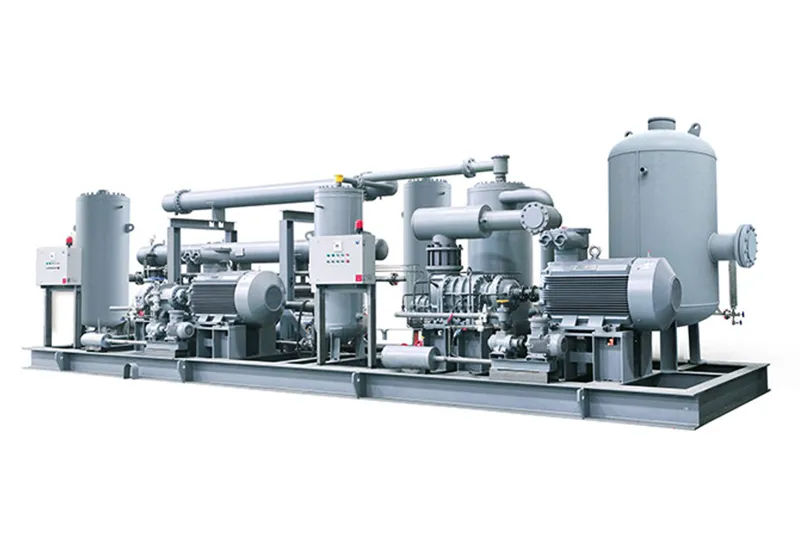
The refrigeration system combines R507/CO₂ cascade refrigeration with a secondary refrigerant system and is divided into multiple circuits for different process requirements, including -42°C quick freezing, -20°C rapid chilling, -8°C air conditioning, and -1°C chilled water. This multi-temperature configuration matches refrigeration capacity precisely to the cooling demands of each processing stage.
The refrigeration system also addresses the technical challenge of condensing CO₂ at ambient temperature. The non-toxic and non-flammable CO₂ also provides important safety advantages in densely staffed processing areas.

MOON-TECH’s EPC capabilities extend beyond refrigeration hardware to intelligent system management. Our independently developed IEMC intelligent energy management system collects process data from the refrigeration circuits and builds mathematical models to support system self-diagnosis and optimized energy management.
The system can automatically adjust the cooling output profile according to local electricity tariff policies, reducing operating costs.
For downstream warehousing and distribution, RFID technology enables full tracking of product information. Combined with an intelligent monitoring system and mobile app, the refrigeration system lets managers check equipment status and cold-storage temperatures anytime, anywhere, keeping the cold chain monitored from the processing workshop through transportation.


The project incorporates energy-saving and environmental measures throughout. Through an integrated heating and cooling system, waste heat from the refrigeration system is recovered and reused to heat defrost water and thaw raw materials, reducing steam consumption.
The workshop roof is also designed to support distributed photovoltaic power generation and solar thermal collection, contributing to the project’s low-carbon operation.
In addition, the project complies with GMP and HACCP standards and uses photolytic oxidation deodorization equipment to treat workshop exhaust, supporting a cleaner, more environmentally responsible, and compliant production process.